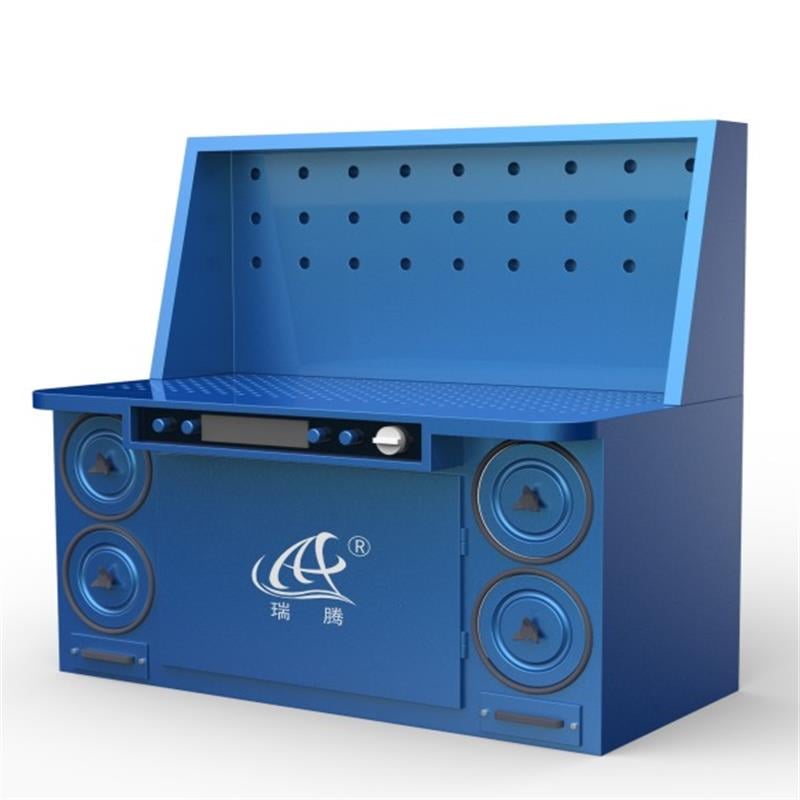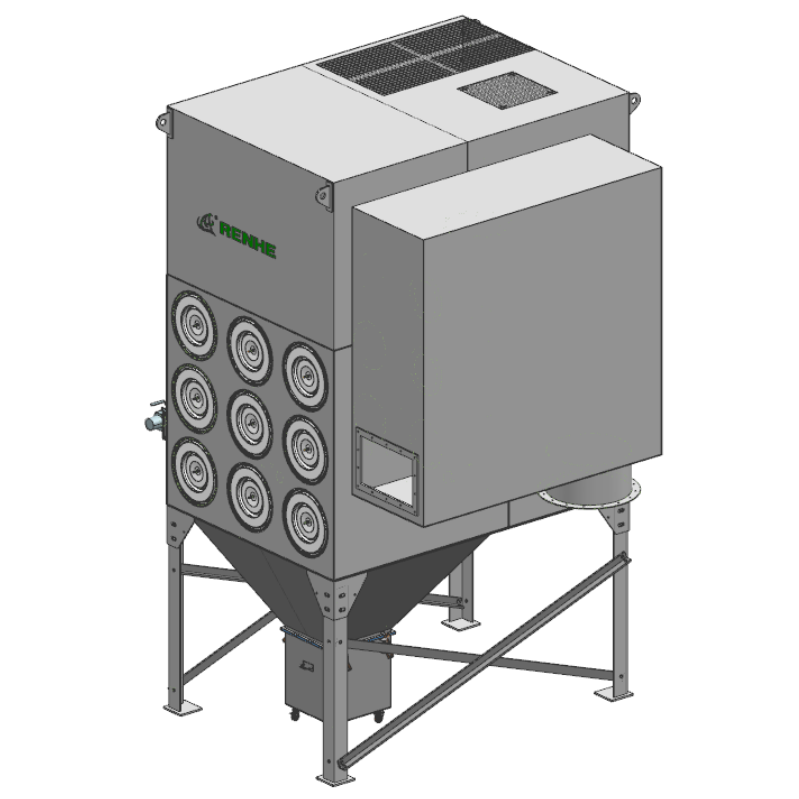
In a workshop with many welding stations, no more than a fraction of them are active at any moment. Yet a conventional fume dust collector often runs one fixed speed fan that pulls air from every hood whether a welder is there or not. That means paying to move conditioned air from idle welding stations all day. The practical question for a plant manager is not whether the fume dust collector can capture smoke, but whether damper control can send suction where it is needed and cut the airflow everywhere else. This guide explains the logic, the zoning decisions, and the checks that make on demand extraction work.
A fan operating against open hoods at every station moves a large, constant airflow. Since fan power rises steeply with airflow, extracting from ten hoods when two are active wastes a substantial share of the energy bill. On demand extraction avoids this waste. The excess airflow also disturbs plant heating and cooling, because makeup air must be tempered. On a fume dust collector without damper control, the only way to reduce extraction is to throttle the whole system, which drops capture at the working stations too. The limitation is not the filter media or the fan but the lack of selective control at the branch level. Any evaluation should separate the cost of moving idle air from the cost of filtering it, because dampers save the former without changing the filter.
Damper control solves this by placing a controllable damper in each branch or zone. When a station is idle, its damper closes and the fan draws from the remaining open branches, so the same fan delivers useful suction to active welding stations. In a modern fume dust collector the dampers are linked to station sensors or work schedules, and a variable speed drive trims the fan to the number of open zones. True on demand extraction needs feedback. The result is on demand extraction: the system follows the work rather than running at full airflow continuously. Pressure sensors confirm that each open hood holds adequate capture velocity, so safety is not traded for savings.
Good zoning is the foundation of reliable damper control. Welding stations that share a process or a bay are grouped, and each zone is sized so that when it is active the remaining open branches still see stable airflow. If too many dampers close at once, the fan can move into an unstable region and capture suffers; the control sequence must keep a minimum number of paths open. A fume dust collector with well designed damper control therefore balances airflow across zones instead of simply shutting branches. Verify that the supplier can show the control sequence, the sensor layout, and the minimum airflow setting, because these details determine whether the system is safe as well as efficient. Document the capture velocity at each hood during a trial so the zoning can be tuned before full rollout.
A useful scenario comes from a multinational heavy industry enterprise producing tower and crawler cranes. On its boom line, large carbon steel components were welded at points that were not fixed, using MAG gas shielded and argon arc processes. A distributed blow and suction arrangement was chosen, with the blow outlet around four metres high and the suction inlet around nine metres high, and the two streams opposed to form a local descending circulation of welding fume. For a fume dust collector serving such a line, damper control matters because different welding stations on the boom are worked at different times. Grouping the capture points into zones and linking dampers to active areas lets the system direct suction to the working section and throttle the rest, cutting airflow without losing capture where sparks and fume are actually generated.
When you compare proposals, look beyond the fan curve. On demand extraction is only as effective as its zoning. Ask how many independent zones the fume dust collector supports, how the dampers fail if power is lost, and whether the control keeps a minimum airflow at open hoods. A manufacturer with more than twenty years in filtration, exports to over sixty countries, and certifications such as CE offers a traceable quality system, but those credentials should support a technical review, not replace it. Request material guidance, review specifications for the control logic, compare product options, and verify test documents before you award a contract. Keep a record of airflow per zone after commissioning; it becomes the baseline for proving the saving.
Question one: Does damper control reduce filtration efficiency?
Answer: No. Filtration efficiency is a property of the media and the seal. Damper control changes how much air reaches the fume dust collector, not how well it filters the air that arrives.
Question two: Can damper control be added to an existing fume dust collector?
Answer: Often yes, if the ducting has distinct branches and the fan can accept a variable speed drive. A site survey should confirm the zoning and the control sequence before retrofit.
Question three: What happens if a damper fails closed at an active welding station?
Answer: Good systems detect the fault and open a backup path or alarm. Ask the supplier to document the failure mode and the minimum airflow rule during review.
 Hot News
2026-11-21
2026-11-21
2026-11-21
2026-11-21
2026-11-21
2026-11-20
Renhe focuses on air filter cartridge, gas turbine air filter, Pleated Filter Media, industrial dust, Our main products have been recognized as high-tech products in Jiangsu Province, famous trademarks in Wuxi City, and CE certification.
NO. 31 Xingyuan Road, Jiefang Industrial Park, Gushan Town, Jiangyin City, Jiangsu Province, China (214414)
Copyright © 2024 Jiangsu Renhe Environmental Equipments Co., Ltd Privacy Policy
 EN